Thin sheet, cosmetic seam
Laser welding with a fixed or robot-carried head, tight clamping and a clean joint gap. The cost sits in the fixture and gap control, not in laser power.
We are an integrator. What we quote is a configuration built around your part, not a catalogue model with a list price. This page explains what moves the number, which brands we supply, and which layout fits which job.
| Line item | What is being specified | What moves the cost |
|---|---|---|
| Robot arm | Payload, reach and whether the arm carries the torch only or the whole laser head | Reach at the far end of the part |
| Laser source | Power, beam quality and duty cycle | Thickness and speed you need to hold |
| Welding power source | Brand, output range and duty cycle of the MIG/MAG source | Wire diameter, plate thickness and arc-on time per shift |
| Torch cooling (water tank) | Cooling capacity, and whether it is built into the source or a separate unit | Duty cycle and how hot the torch runs |
| Seam-tracking sensor | Line-laser vision sensor and controller that finds and follows the weld joint | Joint fit, gap variation and torch standoff |
| Welding head and optics | Focus length, shielding gas design, wire feed option | Joint access and whether filler wire is needed |
| Positioner and fixture | Weight capacity, number of stations, clamping design | Part size and how it is loaded |
| Safety package | Guarding, light curtains, interlocks, CE documentation | Country of installation and existing line layout |
| Fume extraction | Capture hood and filtration class | Coated or galvanized material |
| Integration and commissioning | Programming, operator training, try-out at your plant | How many part numbers and how complex the seams are |
| Service and spares | Response time, spare parts stock, remote support | Uptime target for the line |
No prices are published here on purpose: the same laser power can be quoted at very different totals once fixture, handling and safety are included. Ask for a scoped quote.
Only brands we can actually deliver and support are listed, grouped by the scope they cover in a cell. Product images come from each manufacturer's own website and are stored locally on this site. Model and configuration are fixed per project and quoted individually.
| Brand | Public positioning | Models we quote |
|---|---|---|
| Welding power source and torch cooling (water tank) | ||
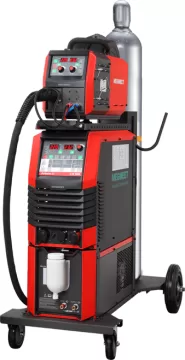 Megmeet (麦格米特) | Listed power-electronics manufacturer (Shenzhen, SZ: 002851) with a dedicated welding division building full-digital inverter welding power sources. | model confirmed per cell |
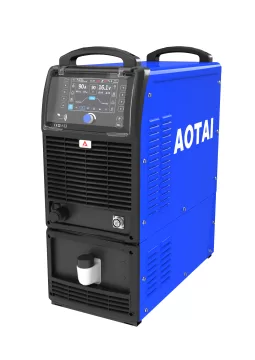 Aotai Electric (奥泰电气) | Jinan-based inverter welding and cutting equipment manufacturer; supplies welding power sources and water-cooling units. | model confirmed per cell |
| Seam-tracking laser sensors | ||
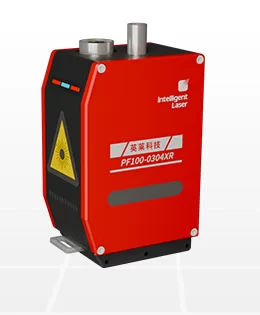 Yinglai (英莱科技) | Founded 2013 in Tangshan; laser vision seam-tracking sensors for industrial robots and welding special machines. | model confirmed per cell |
image to be addedSmartImageAI (明图智能) | Founded 2021 in Suzhou; 3D laser vision sensors for robot welding, cutting and grinding guidance. | model confirmed per cell |
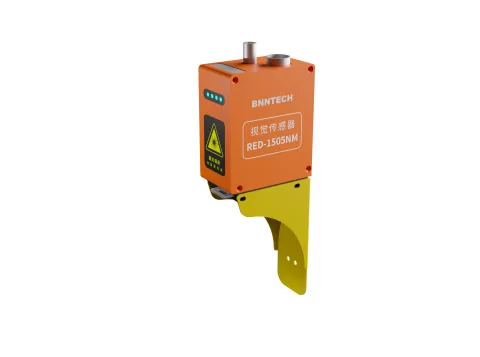 BNNTECH (贝努智能) | Suzhou machine-vision company producing laser seam-tracking sensors; part of the Yinglai group. | model confirmed per cell |
| Collaborative welding robot arms | ||
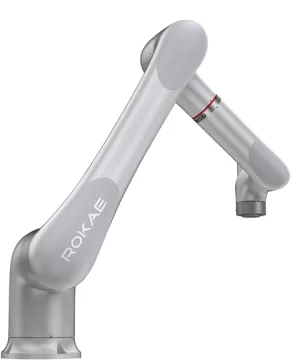 ROKAE (珞石) | Collaborative robot manufacturer; 6-axis arms used for arc and laser welding cells. | model confirmed per cell |
 Dobot (越疆) | Shenzhen-based collaborative robot manufacturer; welding-ready 6-axis arms. | model confirmed per cell |
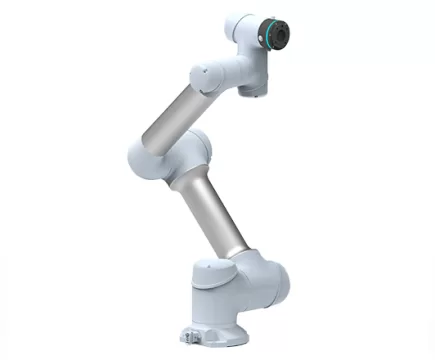 DUCO (多可) | Collaborative robot brand of Siasun (Shenyang); arms used in welding workstations. | model confirmed per cell |
image to be addedESTUN (埃斯顿) | Nanjing-based robot maker with in-house motion control; industrial and collaborative arms used in welding. | model confirmed per cell |
image to be addedAUBO (遨博) | Beijing-based collaborative robot manufacturer; lightweight 6-axis arms used in welding applications. | model confirmed per cell |
The laser source brand is not fixed yet and will be added here once confirmed. Which unit goes into a given cell is decided at the configuration stage and written into the quotation.
Laser welding with a fixed or robot-carried head, tight clamping and a clean joint gap. The cost sits in the fixture and gap control, not in laser power.
MIG/MAG with seam tracking, or laser-arc hybrid when distortion has to stay low. Positioner capacity and travel path dominate the price.
Rotary positioner plus MIG/MAG, or small laser cells for thin-wall tube. Changeover time between part numbers is usually the deciding factor.
Tell us the part, the joint and the volume. We come back with a cell layout and a measured basis for the quote.